


Company Profile
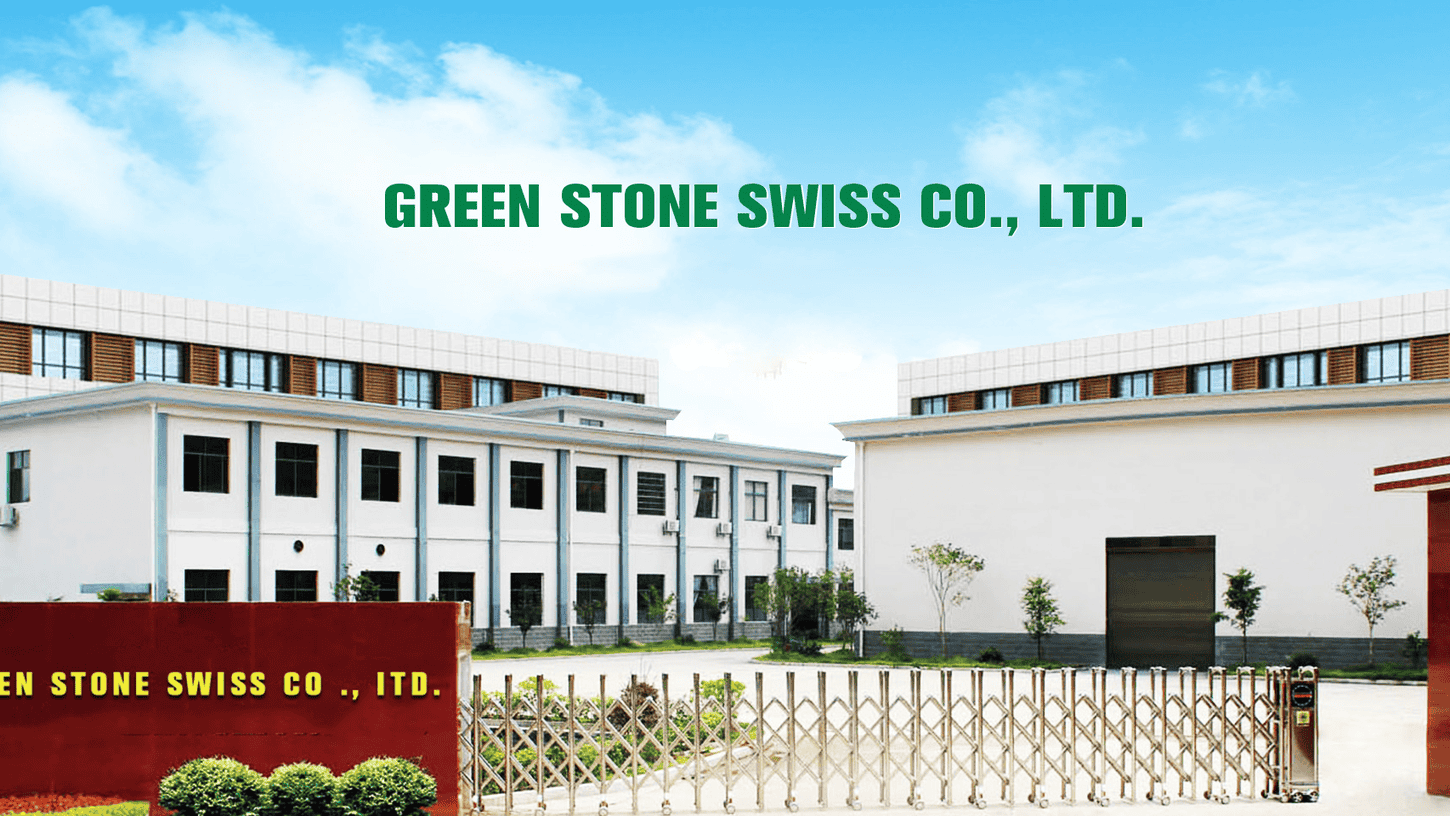
Founded in 2006, Green Stone Swiss Co., Ltd. is a high‑tech enterprise focusing on R&D, production and direct sales of pharmaceutical, nutritional and cosmetic skincare ingredients. Our production‑warehousing base is located in Longgang, Shenzhen. With Hong Kong import‑export qualifications, we provide customized solutions as well as OEM/ODM services.
Our products are sold globally, covering Europe & America, Australia & New Zealand, Southeast Asia, Japan and South Korea. We have served over 100 clients, mainly health supplement manufacturers, skincare factories and overseas professional wholesalers.
Our 12,000‑square‑meter facility is equipped with 5 production lines, supercritical CO₂ extraction system and complete HPLC, GC, UV testing instruments. We devote 30% of revenue to R&D and hold 2 software copyrights, maintaining technical cooperation with multiple domestic and overseas universities & research institutes.
Upholding the principle of *“technological innovation, excellent quality, green and healthy, for the benefit of mankind”*, we supply hundreds of premium raw‑materials across peptides, cosmetic ingredients, plant extracts, nutritional active ingredients and pharmaceutical intermediates for worldwide partners.
Expand Content
Our products are sold globally, covering Europe & America, Australia & New Zealand, Southeast Asia, Japan and South Korea. We have served over 100 clients, mainly health supplement manufacturers, skincare factories and overseas professional wholesalers.
Our 12,000‑square‑meter facility is equipped with 5 production lines, supercritical CO₂ extraction system and complete HPLC, GC, UV testing instruments. We devote 30% of revenue to R&D and hold 2 software copyrights, maintaining technical cooperation with multiple domestic and overseas universities & research institutes.
Upholding the principle of *“technological innovation, excellent quality, green and healthy, for the benefit of mankind”*, we supply hundreds of premium raw‑materials across peptides, cosmetic ingredients, plant extracts, nutritional active ingredients and pharmaceutical intermediates for worldwide partners.

Our Advantages
1. Stable High‑quality Raw‑material Supply Chain
Our China branch is a representative member of The Herbal Materials Association of China. We adopt standardized raw‑material screening and access rules to stabilize upstream quality and reduce batch‑to‑batch fluctuations.
2. Authoritative University‑Industry Technical Cooperation
We have signed technical cooperation agreements with 7 well‑known institutions including University of Sydney, University of Melbourne, Biology Research Institutes of the Science Academy of China and Peking University, to continuously optimize our extraction and synthesis technologies.
3. Rigorous Full‑process Quality Inspection
All active ingredients go through strict HPLC, GC or UV testing before delivery. Purity and impurity indicators are fully verified to satisfy quality standards of overseas health‑care and cosmetic manufacturers.
4. Proprietary Core Production Technologies
We apply advanced supercritical CO₂ extraction for high‑purity output. Our proprietary nanoscale small‑molecule technology delivers smaller‑molecule raw materials for better absorption compared with similar products.
5. Large‑scale Production & Flexible Customization
With 12,000‑㎡ plant, 5 production lines and annual turnover of USD 20,000,000, we support bulk global orders. OEM/ODM and specification customization are available, with MOQ as low as 1 kg for both large factories and small‑medium traders.
6. Mature Global Export & After‑sales Service
Supported by Hong Kong import‑export qualification, we offer sea freight, air freight and courier delivery worldwide with customizable packaging. We provide re‑analysis and product replacement for quality problems caused by our side.
Expand Content
Our China branch is a representative member of The Herbal Materials Association of China. We adopt standardized raw‑material screening and access rules to stabilize upstream quality and reduce batch‑to‑batch fluctuations.
2. Authoritative University‑Industry Technical Cooperation
We have signed technical cooperation agreements with 7 well‑known institutions including University of Sydney, University of Melbourne, Biology Research Institutes of the Science Academy of China and Peking University, to continuously optimize our extraction and synthesis technologies.
3. Rigorous Full‑process Quality Inspection
All active ingredients go through strict HPLC, GC or UV testing before delivery. Purity and impurity indicators are fully verified to satisfy quality standards of overseas health‑care and cosmetic manufacturers.
4. Proprietary Core Production Technologies
We apply advanced supercritical CO₂ extraction for high‑purity output. Our proprietary nanoscale small‑molecule technology delivers smaller‑molecule raw materials for better absorption compared with similar products.
5. Large‑scale Production & Flexible Customization
With 12,000‑㎡ plant, 5 production lines and annual turnover of USD 20,000,000, we support bulk global orders. OEM/ODM and specification customization are available, with MOQ as low as 1 kg for both large factories and small‑medium traders.
6. Mature Global Export & After‑sales Service
Supported by Hong Kong import‑export qualification, we offer sea freight, air freight and courier delivery worldwide with customizable packaging. We provide re‑analysis and product replacement for quality problems caused by our side.
Development Milestones
Foundation · Raw‑material R&D Initiation (2006)
Green Stone Swiss Co., Ltd. was founded. We entered plant extracts and nutritional active raw‑material sectors, built basic R&D & production capacity and established our original mission of technological innovation and green health.
Complete Raw‑material Supply‑chain System
We became a representative member of The Herbal Materials Association of China. Standardized upstream raw‑material screening and management procedures were built to guarantee source‑side raw‑material quality.
Launch of University‑industry Cooperation
We established technical partnerships with multiple top universities and research institutes home and abroad, converting cutting‑edge academic achievements into practical product development.
Production & QC System Full Upgrade
Our 12,000‑㎡ modern production base and 5 production lines were put into operation. Full‑set testing devices were introduced. Supercritical CO₂ extraction and proprietary nanoscale small‑molecule technology realized industrial‑scale application; a complete end‑to‑end quality control system was formed.
Global Business Layout
Official website pharmaceutical‑[sale.net](https://sale.net) went online. Relying on Hong Kong import‑export qualifications, we expanded our overseas market and launched OEM/ODM services for global health‑supplement and skincare manufacturers.
R&D‑driven Sustained Growth
We raised R&D investment to 30% of revenue and kept expanding product lines covering peptides, cosmetic and pharmaceutical ingredients. We keep delivering high‑quality active raw‑materials for global customers under green R&D & manufacturing concept.
Expand Content
Green Stone Swiss Co., Ltd. was founded. We entered plant extracts and nutritional active raw‑material sectors, built basic R&D & production capacity and established our original mission of technological innovation and green health.
Complete Raw‑material Supply‑chain System
We became a representative member of The Herbal Materials Association of China. Standardized upstream raw‑material screening and management procedures were built to guarantee source‑side raw‑material quality.
Launch of University‑industry Cooperation
We established technical partnerships with multiple top universities and research institutes home and abroad, converting cutting‑edge academic achievements into practical product development.
Production & QC System Full Upgrade
Our 12,000‑㎡ modern production base and 5 production lines were put into operation. Full‑set testing devices were introduced. Supercritical CO₂ extraction and proprietary nanoscale small‑molecule technology realized industrial‑scale application; a complete end‑to‑end quality control system was formed.
Global Business Layout
Official website pharmaceutical‑[sale.net](https://sale.net) went online. Relying on Hong Kong import‑export qualifications, we expanded our overseas market and launched OEM/ODM services for global health‑supplement and skincare manufacturers.
R&D‑driven Sustained Growth
We raised R&D investment to 30% of revenue and kept expanding product lines covering peptides, cosmetic and pharmaceutical ingredients. We keep delivering high‑quality active raw‑materials for global customers under green R&D & manufacturing concept.

